Manufacturing Simulation & Operations Research Consulting

Manufacturing simulation that
proves itself before it predicts.

ChiAha builds simulation models of production lines, plants, and supply chains — and validates every one against your own production data before anyone uses it to make a decision. Capacity, bottlenecks, buffers, line design, OEE, networks, staffing: the questions that are too expensive to answer by trial and error on the plant floor.

~1%
OEE Accuracy
300+
Organizations Served
1990
Discrete Rate Simulation Created
35+
Years OR Expertise
What Manufacturers Bring Us

The questions a spreadsheet
can’t answer honestly.

Averages hide interactions. A production line is a coupled system: a stop on one machine starves the next and blocks the one before it, and a buffer in between changes the whole picture. Simulation modeling is how you see those interactions before you spend money on them.

01 / Capacity

Can the line make the plan?

What the plant will actually produce under next year’s mix, a new shift pattern, or a 20% demand increase — and where it breaks first.

02 / Bottlenecks

Which fix actually moves throughput?

The loss tree points at the machine with the most downtime. In the cascade example we publish, that is the Labeler — but 120 one-minute micro-stops on the Filler cascade through the system, and eliminating them recovers 62% more throughput than fixing the Labeler.

03 / Buffers

How big should the buffer be?

Accumulation decouples machines. Too little and every stop propagates; too much and you have paid for floor space and inventory that does nothing. Simulation finds the knee.

04 / Line Design

Will the capital project deliver?

New equipment, a consolidated line, a new product: test the configuration before the purchase order, and check whether the stated ROI survives contact with the rest of the line.

05 / OEE

Where is the hidden factory?

OEE tells you how much you are losing; it doesn’t tell you which losses are recoverable or in what order. A validated model ranks improvements by what they return at the end of the line, not at the machine.

06 / Supply Chain

Is the network right?

Inventory allocation, safety stock, run lengths, and distribution design — modeled as a system over time, pairing optimization with simulation to test what an optimizer proposes.

07 / Staffing

How many people, where, and when?

Operators, maintenance crews, and service lines are queues. M/M/c models and simulation size staffing against service levels when arrivals don’t follow the average.

08 / Something else

Not on the list?

If the decision is expensive and the system is too coupled to reason about on paper, it is probably a modeling problem. Tell us about it.

Schedule a call →
Run It Yourself

The same engine,
in ReliaSim.

The production line models we build for clients run on ReliaSim, our manufacturing simulation software. Its free sandbox runs curated bottling-line models in your browser, including buffer sizing and the loss/gain tradeoff, with an AI assistant that answers from the engine's results.

When you're ready to model your own line, the full version does that, and we can train your team or build the first model with you.
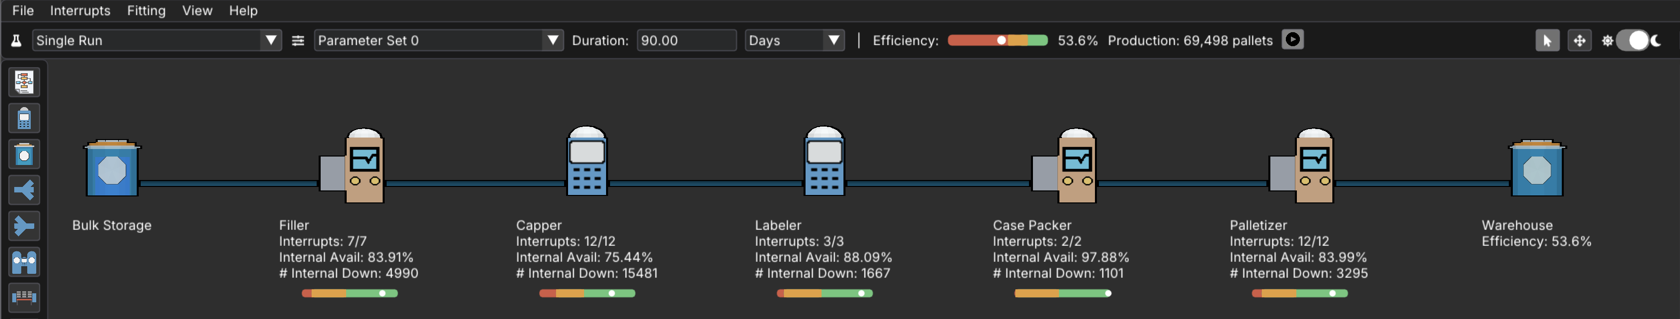
ReliaSim running a bottling line: Filler, Capper, Labeler, Case Packer and Palletizer, with availability and downtime counts for each machine
How an Engagement Runs

From raw data to a model
you can defend.

Every engagement follows the same order: data, then a validated model, then decisions. A model that hasn’t reproduced the past has no business predicting the future.

1

Frame the decision

A capital request, a capacity commitment, an improvement roadmap. We scope the model to answer that decision, not to model everything.

2

Assemble the data you already have

Historian downtime records, machine rates, buffer capacities, product mix, schedules. Failure and repair times are fitted per failure mode where the data supports it; gaps are flagged, never silently defaulted.

3

Build the model in the right paradigm

Discrete rate simulation for high-speed, high-volume, and bulk flow lines; discrete event simulation where individual items matter; optimization and queueing where the question calls for them.

4

Validate against history

The model must reproduce what the system actually did — OEE, throughput, blocking and starving, availability by failure mode — before it is allowed to predict anything. This is the gate, and we show you the comparison.

5

Run the experiments

Hundreds of what-if scenarios instead of the three you had time for, including sensitivity to the inputs you are least sure of.

6

Hand over the decision — and the capability

You get the recommendation and the evidence. Engagements run on the same engines as our products, so your team can license the tools and keep the model working, we can train your analysts, or we stay on as modeling capacity.

Validation First

Simulations validated against real data
before they make predictions.

At the 2020 Winter Simulation Conference, a peer-reviewed discrete rate and reliability model of a multi-line food plant matched a full year of measured OEE to within one percentage point, failure mode by failure mode. A single overall number can be right for the wrong reasons, and a mode-by-mode check can’t hide that.

That model was later rebuilt in ReliaSim and independently validated to the same standard. It ran the same one-year simulation roughly 1,200× faster than the original ExtendSim model on the same laptop. Read the published-validation case study, or see the team’s papers since 1995.

“Those 120 one-minute interruptions are creating cascading problems throughout your system that don’t show up under the original problem’s name. When you eliminate them, you often recover 180–220 minutes of uptime — significantly more than the original downtime suggests.”
Tom Lange · Co-author, “High Accuracy Discrete Rate and Reliability Modeling” (WSC 2020)
Customers

300+ organizations
since the early 1990s.

EssityKellogg’sRich ProductsGeneral MillsConAgraTyson FoodsHormelUnileverPfizerBoschBoeingJTEKTTeleflexSymboticThe Estée Lauder CompaniesHewlett-PackardPitney BowesWalgreensRohm and HaasLindsayBell-Carter FoodsUnion Pacific Railroad

Read what customers said, and 12 published case studies.

Problem → Tool

Other questions,
other tools.

Not every question is about one production line. Here is where each kind of question lives across our tools and guides. Comparing vendors? Start with how to choose manufacturing simulation software.

Your questionWhere to start
Which losses to attack first, and what OEE is really achievable ReliaSimOEE simulation — rank improvements by what they return at the end of the line.
Finding the constraint that actually governs output ReliaSim GuideTheory of constraints simulation — when the bottleneck moves with the failures.
Whether a block-diagram availability calculation is good enough ReliaSim GuideReliability block diagram vs. simulation — what multiplying availabilities misses about buffers. Or have us run a RAM analysis.
Turning downtime logs and historian exports into model inputs ReliaStatsDowntime data analysis — fit time-to-failure and time-to-repair distributions.
High-speed, high-volume, and bulk flow systems DiscreteRateDiscrete rate simulation — the rate-based paradigm, explained with runnable examples.
Queues, service lines, and staffing levels QueueSimQueueing simulation — M/M/c models for staffing against service levels.
FAQ

Manufacturing simulation,
plainly answered.

What is manufacturing simulation?

A computer model of a production line, plant or supply chain that reproduces how the system behaves over time: machines failing and recovering, buffers filling and draining, units starving and blocking. Because it captures those interactions, it answers questions a spreadsheet or downtime Pareto cannot, such as which improvement actually moves throughput.

How is simulation consulting different from buying simulation software?

Software gives your team the capability; consulting gives you the answer and the model behind it. We can build and validate the model, train your analysts to build their own, or both, and engagements run on the same engines as our products. If you are evaluating tools, our buyer’s guide to simulation software lists the questions worth asking.

What data do you need to build a manufacturing simulation model?

Usually data the plant already keeps: downtime or line event data from the historian, machine rates, buffer capacities, product mix and schedule. Failure and repair times are fitted into distributions, per failure mode where the data supports it. Missing inputs are flagged and agreed, never quietly assumed.

How do you validate a simulation model?

Before it predicts anything, the model must reproduce what the system actually did over a historical period: OEE, throughput, and availability by failure mode, not just one aggregate figure that can match for the wrong reasons. Our production models are validated to within about 1% OEE.

What is the difference between discrete event and discrete rate simulation?

Discrete event simulation tracks individual items, so high-speed models run slowly. Discrete rate simulation, created by Andrew Siprelle in 1990 and originally called bulk flow, models flow rates and only fires events when a rate changes, which suits high-speed, bulk and process lines. We use whichever paradigm fits the problem.

Do you do supply chain and operations research work beyond production lines?

Yes. The team has published on supply chain simulation, inventory allocation, safety stock and logistics network design since the late 1990s. We also apply optimization to network design, M/M/c queueing models to staffing, reliability statistics to downtime data, and theory of constraints to finding the real bottleneck.

Next Step

Bring us the question
you can’t afford to guess.

Tell us about the line, the plant, or the network and the decision in front of you. We’ll tell you honestly whether simulation is the right tool — and what it would take to get a validated answer.

Schedule a call Try the ReliaSim sandbox